Leave Your Message

10 Tips for Choosing the Best Folding Paper Box?

Choosing the right Folding Paper Box is no longer a purely visual decision. Packaging now influences product protection, shipping efficiency, brand trust, and environmental claims. A box that looks premium on a screen may arrive crushed, scuffed, or difficult to recycle.

Industry data supports closer evaluation. Smithers’ report, The Future of Folding Cartons to 2029, identifies continued demand for lightweight, printable, and recyclable carton formats. Meanwhile, Eurostat reported that paper and cardboard packaging recycling reached approximately 82% in the European Union in 2022. These figures show the market’s direction, but they do not make every paper box sustainable. Board source, coatings, inks, adhesives, and local recycling systems still matter.

Details matter. The ten tips in this guide examine board grade, GSM, caliper, folding accuracy, dieline design, printing quality, closure strength, moisture resistance, supplier certification, and total cost. Sample testing should include stacking, drop, vibration, and humidity exposure. A small box can fail under surprising pressure. A beautiful finish can also reduce recyclability or increase production waste.

Not every specification tells the full story. FSC certification may support responsible sourcing, but it does not guarantee perfect manufacturing. Recycled paper may reduce virgin fiber demand, yet it can require stronger structure or careful surface treatment. The practical answer is balance: protect the product, communicate the brand, control costs, and verify environmental claims with documented evidence. Choosing well takes more than a catalogue image.

10 Tips for Choosing the Best Folding Paper Box?

Set Specifications: 250–600 gsm Board, Caliper, Dimensions, and Load

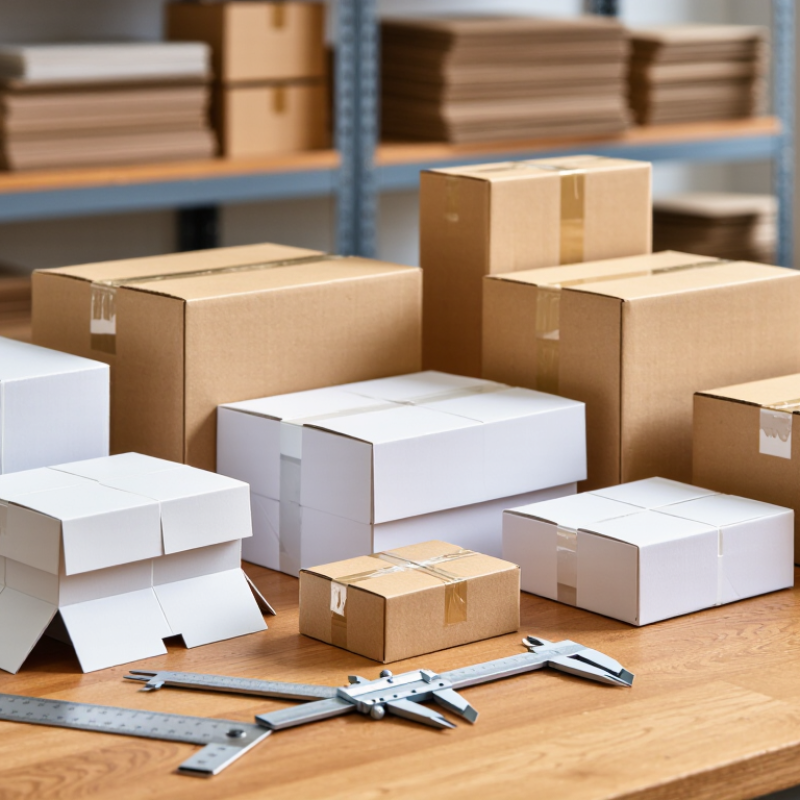
A folding paper box should begin with measurable specifications, not attractive artwork. Board weight between 250 and 600 gsm covers many retail applications. Yet gsm alone does not predict durability. A 350 gsm folding board may measure approximately 0.45–0.60 mm, while 600 gsm stock can approach or exceed 0.80 mm. Fibre type, coating, moisture, and calendering change the result. Measure caliper under ISO 534 conditions, then request production samples. Small differences matter.

Start with internal dimensions, not the flat dieline. Record length, width, and depth in millimetres. Allow space for the product, inserts, and folding tolerance. Load testing should reflect real use. A box holding 2 kilograms on a warehouse pallet needs different performance from a box carrying 200 grams by hand. Compression, stacking time, humidity, and corner strength should be tested. The United Nations FAO Forestry Production and Trade data reports global paper and paperboard production above 400 million tonnes annually, but scale does not guarantee consistent board quality. I have seen specifications look perfect on paper and fail after moisture exposure. That is the part worth questioning. Use test results, not assumptions. Cite: ISO 534:2011; UN FAO Forestry Production and Trade Database, 2023.

Compare Board Performance with ISO 536 Grammage and ISO 534 Caliper Tests

Choosing the best folding paper box starts with measurable board performance, not appearance alone. ISO 536 determines grammage in grams per square metre (g/m²). ISO 534 measures caliper, or sheet thickness, in micrometres. Together, these tests reveal whether a board feels strong, folds cleanly, and fits the intended product.

Tip: Request a laboratory test report before approving samples. A 350 g/m² board may feel substantial, but its caliper can vary by fibre mix, coating, and manufacturing process. Two boards with identical grammage may therefore stack differently or resist creasing differently. ISO 534 helps expose that difference. Measure several sheets, not one. Paper is not perfectly uniform.

The Food and Agriculture Organization reported global paper and paperboard production above 400 million tonnes in recent forestry statistics, showing the scale of material selection. Yet higher grammage does not automatically create a better box. Excess thickness can cause cracking along folds, poor closure, and inefficient transport.

Tip: Compare grammage, caliper, folding behaviour, and compression results together. Use samples from the same production batch. Record moisture and test conditions, because humidity can change board stiffness and dimensions. The International Organization for Standardization provides test methods, not universal pass limits. Set limits based on box size, crease design, filling weight, and shipping stress.

One practical mistake is trusting a single “premium” specification. Real packaging performance often depends on several modest values working together. Test more than seems necessary.

Check Crease Accuracy, Locking Style, and Prototype Fit Before Production

Choosing the best folding paper box starts with measurable details, not attractive drawings. Check whether crease lines are sharp, centered, and consistent across the sheet. A crease that shifts by two millimeters can make a lid sit unevenly. Inspect folded samples under normal warehouse lighting. Small defects often disappear in digital artwork.

Locking style also affects speed, strength, and customer use. Tuck flaps suit simple packaging, while crash-lock bases support heavier products. Test each lock with repeated opening and closing. It should hold firmly without tearing the paper fibers. Too tight is a problem. Operators may struggle during packing. Too loose can cause boxes to open during handling.

Prototype fit must be tested with the actual product, including inserts, labels, and protective materials. Measure clearance at every corner. A box may fit an empty sample but fail when filled. I once approved a prototype that looked accurate, yet its product shifted during transport testing. That mistake showed me the value of practical trials. Use several prototypes, not one lucky sample. Record dimensions, folding pressure, closure performance, and visible stress marks before production. Ask an experienced packaging technician to review the die line and sample together. Their comments may challenge your original choice, which is useful. Good packaging decisions come from evidence, careful testing, and a willingness to revise.

10 Tips for Choosing the Best Folding Paper Box? - Check Crease Accuracy, Locking Style, and Prototype Fit Before Production

No. Evaluation Dimension What to Check Practical Acceptance Guidance Why It Matters Before Production
1 Board Grade and Thickness Confirm the paperboard type, grammage, thickness, stiffness, and suitability for the product weight. The selected board should support the filled product without excessive bending, crushing, or panel deformation. Verify the specification on the technical data sheet. Board variation can affect folding performance, box strength, print registration, and the final internal dimensions.
2 Crease Accuracy Inspect whether crease lines are straight, continuous, correctly positioned, and compatible with the board grain and thickness. Folded panels should meet cleanly without splitting, whitening, cracking, or visibly drifting away from the intended fold positions. Inaccurate creases can cause crooked boxes, poor lid alignment, unstable corners, and a difficult packing process.
3 Locking Style Compare tuck-end, snap-lock, crash-lock, auto-bottom, and other locking structures for assembly and opening requirements. The lock should close securely, open without excessive force, and remain engaged during handling, transport, and shelf display. An unsuitable lock may increase assembly time, cause accidental opening, or require additional adhesive and labor.
4 Prototype Fit Place the actual product, insert, leaflet, and protective components inside a physical prototype. The contents should fit without damaging the product or causing excessive empty space. Allow practical clearance for manufacturing and packing variation. A digital dieline cannot fully reveal interference, product movement, insertion difficulty, or removal problems.
5 Dieline and Panel Dimensions Review overall dimensions, glue flaps, dust flaps, tuck flaps, corner clearances, and panel relationships in the cutting layout. The dieline should use consistent units, clearly marked cut and crease lines, and sufficient flap overlap for reliable assembly. Small dimensional errors can become visible gaps, crushed edges, or locking failures after folding.
6 Print Registration and Bleed Check artwork alignment against cut and crease lines, minimum margins, barcode placement, and bleed around cut edges. Keep critical text, logos, barcodes, and legal information away from cut and crease lines; use a print-ready file with defined bleed. Poor registration may cut into important information or create uneven borders and unattractive finished panels.
7 Surface Finish and Coating Evaluate uncoated, coated, matte, gloss, varnished, or laminated surfaces for appearance, handling, and fold performance. The finish should resist expected scuffing and moisture exposure without cracking excessively along creases or interfering with glue adhesion. A finish that is too brittle, slippery, or poorly bonded can reduce visual quality and assembly reliability.
8 Glue Joint Performance Inspect the glue flap width, adhesive coverage, bond strength, curing condition, and visible squeeze-out. The joint should remain closed during normal handling and should not show exposed adhesive, warping, or delamination. Weak or misaligned glue joints can cause open seams, distorted boxes, packing interruptions, and product loss.
9 Assembly and Packing Efficiency Time the manual or machine assembly process and check whether products can be inserted and removed smoothly. The structure should assemble consistently with minimal rework and should be compatible with the intended packing equipment or workflow. A box that looks attractive but assembles slowly can increase labor cost and reduce production throughput.
10 Transport and Quality Testing Test filled boxes for compression, vibration, drop handling, stacking, humidity exposure, and repeated opening where applicable. Define test conditions based on product weight, distribution route, stacking pattern, and expected storage environment before approving mass production. Testing helps identify structural weakness, abrasion, deformation, and accidental opening before large quantities are manufactured.

Pre-production rule: Approve the physical prototype, final dieline, material specification, artwork proof, assembly method, and quality criteria before releasing the production order.

Validate Color, Coatings, and Food Contact Against ISO 12647 and FDA Rules

Color is not decoration alone; it signals quality before a customer opens the folding box. Smithers’ recent folding-carton market review places global demand above US$100 billion, increasing pressure on printers to control consistency. Request an ISO 12647 press proof before production. Check substrate whiteness, ink density, dot gain, and acceptable color difference. ISO 12647-2 supports process control for offset printing, but it does not guarantee identical results on every board. That part is often misunderstood.

Coatings require a separate review. Ask for the coating type, curing method, and migration test results. For food packaging, FDA 21 CFR 176.170 addresses paper and paperboard contacting aqueous or fatty foods, while 21 CFR 176.180 covers dry foods. The exact food, temperature, and contact time still matter. Test the finished structure, not only the paper. Include inks, varnishes, adhesives, and recycled fibers. Keep batch records and retain a production sample. Small details matter.

A practical weakness remains. Suppliers may provide a compliance letter without complete test conditions. Treat it as evidence, not proof. Compare the declared use with your real filling line and storage environment. Recheck color after coating, because gloss can make a dull print appear stronger. Human judgment still helps, but it should support measured data, not replace it.

Choose Suppliers Using FSC Certification, MOQ, Lead Time, and Total Cost

Choosing the best folding paper box starts with checking the supplier, not only the sample. FSC certification can show responsible material sourcing, but verify the certificate number, scope, and validity. Ask whether it covers the paper used for your specific boxes. Check the paperwork. A polished certificate image proves little without traceable records.

MOQ affects both budget and inventory risk. A low MOQ may suit product testing, seasonal packaging, or a small launch. However, unit prices can rise because setup, cutting, and printing costs are spread across fewer boxes. Request a clear MOQ table for different sizes, paper grades, and finishes. Samples also matter. A box may fold well on a screen but fail when filled with a heavy product.

Lead time should include artwork approval, sampling, production, quality checks, and shipping. Ask for each stage in writing. Time slips. Build a buffer before a campaign or retail delivery date. Total cost includes tooling, plates, color proofs, packaging, freight, taxes, storage, and possible rework. Compare complete quotations, not just the unit price. An experienced supplier should explain material thickness, folding tolerance, and inspection standards in practical terms.

I once underestimated storage costs because the quoted price looked attractive. That mistake changed the real margin. Require a pre-production sample, confirm carton dimensions, and record agreed specifications before payment.